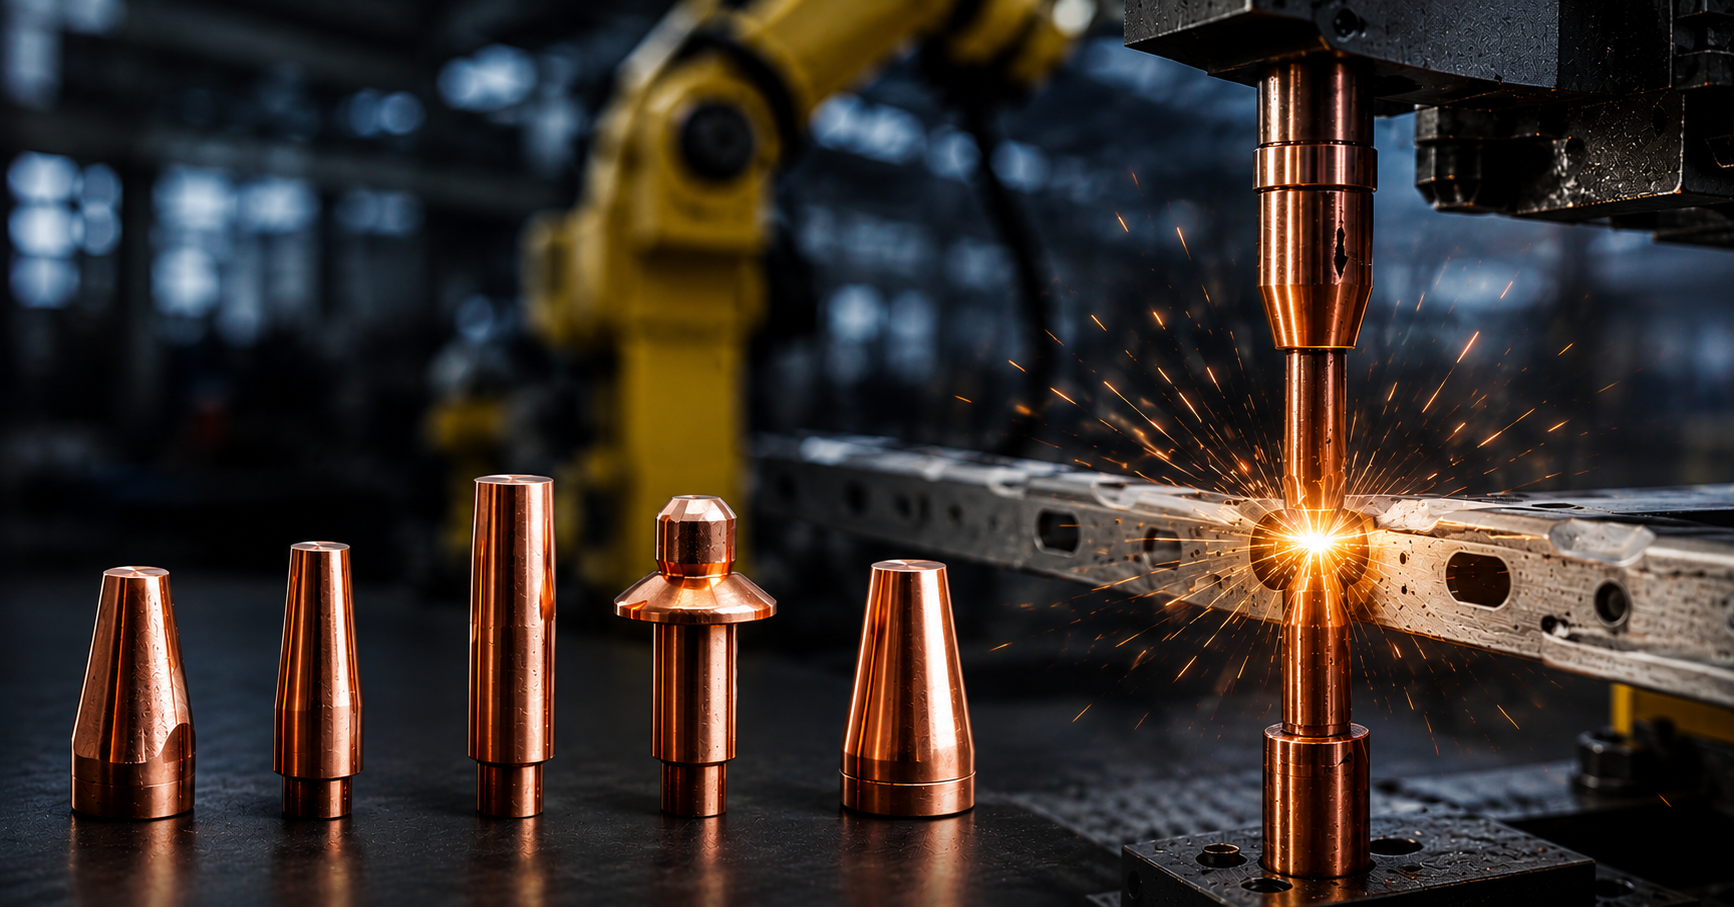
Resistance welding electrode selection is a material-driven decision that directly determines process stability, maintenance frequency, and weld consistency. Electrode performance is not defined by nominal welding parameters alone. It is defined by how consistently the electrode maintains its contact geometry and surface condition under repeated thermal and mechanical loading.In production environments, electrode degradation typically occurs through a combination of deformation, surface degradation, and thermal fatigue. These mechanisms are directly linked to measurable material properties such as electrical conductivity (% IACS), hardness (HBW), and thermal conductivity (W/m·K). As these properties vary, the balance between heat generation and heat dissipation shifts at the electrode interface, altering current density and accelerating wear.
This guide provides a structured framework for selecting AMPCOLOY® and AMPCO® alloys based on welding process, base material, and dominant wear mechanism. It is intended to support specification decisions prior to RFQ by translating material properties into predictable production behavior.
For a more comprehensive look at the role of High-Conductivity Alloys see our technical paper
"Performance and Wear Mechanisms of High-Conductivity Alloys in Resistance Welding".
Summary: What to Select
Resistance welding electrode selection is governed by the interaction between electrical conductivity, mechanical strength, and thermal stability under cyclic loading.
- For mild steel spot welding, RWMA Class 2 alloys such as AMPCOLOY® 972 (~65–70% IACS) provide high electrical conductivity.
- For stainless steel applications, RWMA Class 3 alloys such as AMPCOLOY® 95 (~48–55% IACS, ~200 HBW) and AMPCOLOY® 940 (~45–50% IACS, ~210 HBW) provide improved resistance to thermal softening and deformation.
- For flash butt welding and high-force applications, AMPCOLOY® 83 (380 HBW, 22% IACS, ~106 W/m·K) provides higher mechanical strength and maintains contact stability under load.
Decision Matrix:
Process, Constraint, and Alloy Selection
The following matrix maps welding process conditions to the dominant constraint and corresponding AMPCO alloy selection. Final confirmation requires alignment with process parameters and observed wear behavior.
|
Welding Process |
Base Material |
Dominant Constraint |
Recommended Alloy |
Key Property Driver |
|
Spot Welding |
Mild Steel |
Heat accumulation |
AMPCOLOY® 972 |
~65–70% IACS conductivity |
|
Spot Welding |
Stainless Steel |
Deformation |
AMPCOLOY® 95 |
~200 HBW hardness |
|
Seam Welding |
Mild Steel |
Thermal stability |
AMPCOLOY® 972 |
Heat dissipation |
|
Seam Welding |
Stainless Steel |
Wear + deformation |
AMPCOLOY® 940 / 95 |
Strength–conductivity balance |
|
Projection Welding |
Mixed |
Force-driven deformation |
AMPCOLOY® 972 / 95 |
Contact stability |
|
Flash Butt Welding |
Steel |
Mechanical load |
AMPCOLOY® 83 |
380 HBW strength |
Identify the Dominant Wear Mechanism
Effective electrode selection begins with identifying the mechanism that limits performance in production:
- Deformation-Driven Wear: This mechanism is characterized by progressive tip growth (mushrooming) under combined temperature and force. As the electrode softens, the contact area increases, reducing current density and shifting heat away from the weld interface. This leads to increased energy input requirements and accelerated wear progression.
Material implication: Prioritize hardness and strength to resist plastic deformation.
- Heat-Driven Softening: This occurs when insufficient heat extraction causes sustained high temperatures at the electrode face. Strength decreases as temperature rises, accelerating deformation even at constant force.
Material implication: Prioritize electrical and thermal conductivity to stabilize heat balance and reduce peak temperature. - Surface-Driven Wear (Pickup and Adhesion): Surface degradation takes place when material transfer, coating interaction, or spatter adhesion alters contact resistance. This leads to localized overheating and instability.
Material implication: Conductivity supports thermal stability, but surface interaction must be controlled through process and geometry.
Identify Your Welding Process
The dominant wear mechanisms described above manifest differently depending on the welding process, as each process imposes distinct thermal and mechanical conditions at the electrode interface. The following sections describe how these conditions influence electrode behavior and material selection.
Spot Welding
Spot welding is characterized by localized current flow through a defined electrode tip geometry. Typical current levels range from 8 to 25 kA, and heat generation follows Joule’s law (Q = I²Rt). Under these conditions, current density is concentrated at the electrode–workpiece interface, and electrode performance depends on maintaining stable geometry and controlled heat flow.
Electrical conductivity determines how much resistive heat is generated within the electrode body relative to the weld interface. Higher conductivity reduces internal heating and stabilizes temperature at the electrode face. Thermal conductivity governs the rate at which this heat is removed through the electrode and cooling system, limiting time spent at elevated temperature where strength decreases.
When welding mild steel, the relatively high conductivity of the workpiece distributes heat more evenly. In this case, electrode performance is primarily limited by heat accumulation and thermal drift. A high-conductivity alloy such as AMPCOLOY® 972 (~65–70% IACS) maintains a stable heat balance and delays the onset of temperature-driven softening.
When welding stainless steel, the significantly lower conductivity of the workpiece concentrates heat at the interface. This increases electrode temperature and accelerates strength loss. Under these conditions, deformation becomes the dominant wear mechanism. AMPCOLOY® 95 (~48–55% IACS, ~200 HBW) provides higher hardness and strength retention, reducing deformation and maintaining tip geometry over longer intervals.
Seam Welding
Seam welding introduces continuous thermal input due to the rolling contact of wheel electrodes. The electrode remains in contact with the workpiece over extended periods, leading to cumulative heat build-up. This shifts the thermal balance compared to spot welding and increases the importance of both thermal conductivity and surface stability.
Electrode wear in seam welding is typically expressed as progressive geometry loss and surface degradation over weld length rather than discrete cycles. As temperature rises, strength decreases, and deformation accelerates. If heat extraction is insufficient, the electrode remains at elevated temperature for longer durations, increasing the rate of wear.
For mild steel applications, AMPCOLOY® 972 provides sufficient electrical and thermal conductivity to maintain a stable temperature profile during continuous operation. For stainless steel or higher thermal load conditions, AMPCOLOY® 940 or AMPCOLOY® 95 provide improved resistance to deformation and maintain geometry under prolonged exposure.
Projection Welding
Projection welding involves larger contact areas and higher compressive forces. The current is distributed across projections that collapse under pressure when melting of materials starts, resulting in a different balance between electrical and mechanical loading compared to spot welding.
Because the contact area between the electrode and workpiece is larger, current density is lower. However, the mechanical loading remains the dominant constraint, increasing the contribution of deformation-driven wear. Under these conditions, hardness and yield strength become more critical than maximum conductivity.
AMPCOLOY® 940 is typically selected for applications where larger contact areas require a balance between conductivity and mechanical stability. For smaller projections or more concentrated loading, AMPCOLOY® 95 provides higher resistance to deformation and maintains contact geometry more effectively.
Flash Butt Welding
Flash butt welding operates under extreme electrical and mechanical conditions, with current levels typically ranging from 40 to 100 kA. In this process, electrodes function as clamping elements that must maintain alignment and contact stability under high force.
The dominant constraint in flash butt welding is mechanical loading combined with localized heating at the interface. Duty cycle/power on time is typically low, allowing extended time to cool down in between welds, which makes the specific heat of the electrode material also important for heat management. Under these conditions, deformation resistance becomes the primary requirement. Electrical conductivity remains relevant, but it is not the dominant selection criterion.
AMPCOLOY® 83 provides a combination of hardness (380 HBW), electrical conductivity (22% IACS), and thermal conductivity (~106 W/m·K) that supports stable operation under high-force conditions. The higher hardness reduces plastic deformation, while moderate conductivity allows controlled heat transfer without excessive internal heating.
Replacement Mapping:
From Existing Materials to AMPCO Alloys
Electrode replacement is typically initiated when production metrics indicate instability. These include increased dressing frequency, accelerated geometry change, and reduced weld consistency. The underlying cause is a mismatch between material properties and the dominant wear mechanism.
|
Current Material |
Typical Limitation |
AMPCO Recommendation |
Measurable Difference |
|
CuAl10Ni |
160 HBW, 8% IACS |
AMPCOLOY® 83 |
380 HBW, 22% IACS |
|
Generic RWMA Class 2 |
Deformation in stainless welding |
AMPCOLOY® 95 |
Higher hardness, Class 3 suitability |
|
Low-conductivity bronze |
Heat accumulation |
AMPCOLOY® 972 |
~65–70% IACS conductivity |
- Increasing hardness from 160 HBW to 380 HBW when replacing CuAl10Ni with AMPCOLOY® 83 improves resistance to plastic deformation under load. Furthermore, increasing electrical conductivity from 8% to 22% IACS reduces resistive heating within the electrode and improves heat transfer during the weld cycle.
- Moving from RWMA Class 2 to Class 3 (AMPCOLOY® 95) increases mechanical strength and hardness (~200 HBW) at the expense of conductivity, which is appropriate when deformation (“mushrooming”) dominates wear. Higher strength maintains the tip geometry over more cycles than a standard Class 2 alloy could.
- Replacing low-conductivity bronze with AMPCOLOY® 972 combats heat-driven softening. By providing a high electrical conductivity of ~65-70% IACS, AMPCOLOY® 972 ensures that less heat is generated within the electrode body and more heat is efficiently dissipated. This stabilizes the temperature at the electrode face and prevents the thermal drift that leads to inconsistent weld nuggets.
Understand Expected Electrode Performance
Material replacement changes how wear develops over time rather than eliminating it. The differences in conductivity, hardness, and thermal behavior directly influence how quickly electrode geometry and surface condition degrade under a given welding schedule.
In production, higher electrical and thermal conductivity reduce heat accumulation at the electrode face, which slows temperature-driven softening and stabilizes contact conditions. This is observed as reduced face growth rate and more consistent intervals between dressing operations. Higher hardness reduces plastic deformation under load, maintaining current density and delaying geometry-driven process drift.
These effects result in more stable weld conditions, extended maintenance intervals, and improved predictability of electrode consumption rather than fixed increases in service life.
Recognize the Consequences
of Incorrect Material Selection
When electrode material properties do not match the dominant wear mechanism, degradation accelerates and process stability decreases.
If conductivity is sufficient but mechanical strength is inadequate, deformation occurs rapidly under load, increasing contact area and reducing current density at weld interface. If strength is high but conductivity is insufficient, heat accumulates at the electrode face, accelerating thermal softening and altering contact conditions. When the electrode is not matched to the base material conductivity, heat distribution shifts away from the weld interface, resulting in inconsistent nugget formation.
These conditions increase dressing frequency, reduce process stability, and shorten usable electrode life under otherwise unchanged welding parameters.
When Should You Change Electrode Material?
Electrode material should be reassessed when process stability begins to drift under otherwise unchanged welding conditions. In production, degradation appears as progressive changes in geometry and surface condition that alter current density and contact behavior over time.
The following conditions indicate that the selected material no longer matches process requirements:
- Dressing intervals decrease despite stable welding parameters
- Electrode tip diameter increases beyond specified tolerance
- Weld nugget size becomes inconsistent under constant current and force
- Cooling system temperature increases during operation
- Workpieces show accelerated deformation or marking
These indicators show that the dominant wear mechanism is no longer adequately controlled by the current material, and that the balance between conductivity and mechanical strength is no longer aligned with process conditions.
Pre-RFQ Technical Checklist
Accurate electrode selection requires a defined set of process parameters. These parameters determine the thermal and mechanical load on the electrode and allow material selection to be aligned with operating conditions.
The following information should be established prior to RFQ:
- Base material grade and surface condition
- Sheet thickness and stack configuration
- Weld current (kA) and welding time (ms)
- Electrode force (kN)
- Cooling water flow rate and inlet temperature
- Current electrode material and RWMA classification
These variables define the heat balance at the electrode interface and determine whether wear is dominated by temperature-driven softening, mechanical deformation, or surface interaction.
Validate Your Electrode Material Selection
If you are evaluating electrode material changes, download our technical paper for a detailed, data-based analysis of wear mechanisms and alloy performance under resistance welding conditions.
For pre-RFQ confirmation, submit your welding parameters for application-specific material selection and electrode design support.