---
title: "Validated Performance in Resistance Welding: Production Results with AMPCOLOY® Electrodes"
description: "Two production case studies: AMPCO® 18 extends electrode reprofiling intervals, AMPCOLOY® Mylar eliminates spatter cleaning in robotic welding."
image: https://academy.ampcometal.com/hubfs/ChatGPT%20Image%20Aug%2024%2c%202026%2c%2004_38_22%20PM.png
---
[](https://academy.ampcometal.com/)
- Products
- AMPCO® Aluminium Bronze
- [AMPCO® 8](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-8/)
- [AMPCO® 15](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-15/)
- [AMPCO® 18](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-18/)
- [AMPCO® 18.136](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-18-136/)
- [AMPCO® 18.22](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-18-22//)
- [AMPCO® 18.23](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-18-23/)
- [AMPCO® 21](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-21/)
- [AMPCO® 22](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-22/)
- [AMPCO® 25](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-25/)
- [AMPCO® 26](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-26/)
- [AMPCO® 45](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-45/)
- [AMPCO® M4](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-m4/)
- AMPCOLOY® High Copper Alloy
- [AMPCOLOY® 83](https://www.ampcometal.com/products/ampcoloy-high-copper-alloy/ampcoloy-83/)
- [AMPCOLOY® 88](https://www.ampcometal.com/products/ampcoloy-high-copper-alloy/ampcoloy-88/)
- [AMPCOLOY® 89](https://www.ampcometal.com/products/ampcoloy-high-copper-alloy/ampcoloy-89/)
- [AMPCOLOY® 91](https://www.ampcometal.com/products/ampcoloy-high-copper-alloy/ampcoloy-91/)
- [AMPCOLOY® 95](https://www.ampcometal.com/products/ampcoloy-high-copper-alloy/ampcoloy-95/)
- [AMPCOLOY® 940](https://www.ampcometal.com/products/ampcoloy-high-copper-alloy/ampcoloy-940/)
- [AMPCOLOY® 944](https://www.ampcometal.com/products/ampcoloy-high-copper-alloy/ampcoloy-944/)
- [AMPCOLOY® 972](https://www.ampcometal.com/products/ampcoloy-high-copper-alloy/ampcoloy-972/)
- [Cu-W Sintered](https://www.ampcometal.com/products/ampcoloy-high-copper-alloy/cu-w-sintered)
- AMS Alloys
- [AMS 4590](https://www.ampcometal.com/products/ams-alloys/ams-4590/)
- [AMS 4640](https://www.ampcometal.com/products/ams-alloys/ams-4640/)
- [AMS 4880](https://www.ampcometal.com/products/ams-alloys/ams-4880/)
- [AMS 4881](https://www.ampcometal.com/products/ams-alloys/ams-4881/)
- [Standard Alloys](https://www.ampcometal.com/products/standard-alloys/)
- [Welding Wire](https://www.ampcowelding.com/)
- [Safety Tools](https://www.safetytools.com/)
- Solutions
- Applications
- [Wear Resistance](https://www.ampcometal.com/applications/wear-resistance/)
- [Corrosion Resistance](https://www.ampcometal.com/applications/corrosion-resistance/)
- [Metal Forming & Tooling](https://www.ampcometal.com/applications/metal-forming/)
- [Die Casting](https://www.ampcometal.com/applications/die-casting/)
- [Plastic Processing](https://www.ampcometal.com/applications/plastic-processing/)
- [Resistance Welding](https://www.ampcometal.com/applications/resistance-welding/)
- Industries
- [Aerospace](https://www.ampcometal.com/industries/aerospace/)
- [Automotive](https://www.ampcometal.com/industries/automotive/)
- [General Engineering](https://www.ampcometal.com/industries/general-engineering/)
- [Marine](https://www.ampcometal.com/industries/marine/)
- [Metal Forming](https://www.ampcometal.com/industries/metal-forming/)
- [Oil, Gas & Chemical](https://www.ampcometal.com/industries/oil-gas-chemical/)
- [Plastic Processing](https://www.ampcometal.com/industries/plastic-processing/)
- [Resistance Welding](https://www.ampcometal.com/industries/resistance-welding/)
- [Steel](https://www.ampcometal.com/industries/steel)
- [Hydrogen](https://www.ampcometal.com/industries/hydrogen)
- [Luxury](https://www.ampcometal.com/industries/luxury)
- [Finished Machine Parts](https://www.ampcometal.com/finished-machined-parts/)
- [Additive Manufacturing](https://www.ampcometal.com/additive-manufacturing/)
- [Technical Consulting](https://www.ampcometal.com/technical-consulting/)
- Who We Are
- [Sustainability](https://www.ampcometal.com/sustainability/)
- [Sustainability Management](https://www.ampcometal.com/sustainability/sustainability-management/)
- [Environment](https://www.ampcometal.com/sustainability/environment/)
- [Social](https://www.ampcometal.com/sustainability/social/)
- [Governance](https://www.ampcometal.com/sustainability/governance/)
- [Future Goals](https://www.ampcometal.com/sustainability/furure-goals/)
- [Our History](https://www.ampcometal.com/our-history/)
- [About Us](https://www.ampcometal.com/about-us/)
- [Working at AMPCO](https://www.ampcometal.com/working-at-ampco)
- [Working with AMPCO](https://www.ampcometal.com/working-with-ampco)
- Technical Hub
- Technical Data
- [Application Datasheets](https://www.ampcometal.com/application-datasheets/)
- [Technical Datasheets](https://www.ampcometal.com/technical-datasheets/)
- [Microcast® Technology](https://www.ampcometal.com/mirocast-technology/)
- [Machining Recommendations](https://www.ampcometal.com/machining-recommendations/)
- Documentation
- [Safety Data Sheets](https://www.ampcometal.com/safety-data-sheets/)
- [Certifications](https://www.ampcometal.com/certifications/)
- [Food Approval Data](https://www.ampcometal.com/food-approval-data/)
- [Sales Terms and Conditions](https://www.ampcometal.com/sales-terms-and-conditions/)
- [ATEX Certification Data](https://www.ampcometal.com/atex-certification-data/)
- [Product Selection Tool](https://www.ampcometal.com/product-selection-tool/)
- [Stock Availability](https://www.ampcometal.com/ssd/)
- [Academy](https://academy.ampcometal.com/)
- [Contact](https://www.ampcometal.com/contact-us/#contact-us)
# Validated Performance in Resistance Welding: Production Results with AMPCOLOY® Electrodes
Oct 7, 2026, 4:35:16 PM | Written by [AMPCO METAL](https://academy.ampcometal.com/author/ampco-metal)
- [Tweet](https://twitter.com/share)
Material selection in welding environments is often validated only after performance limitations become visible in production. These limitations typically appear as increased maintenance intervention, process variability, or reduced equipment availability rather than immediate component failure.
In resistance welding and adjacent welding operations, the interaction between electrical loading, mechanical force, and thermal exposure creates conditions where small differences in material properties produce measurable changes in production behavior. Variations in hardness influence resistance to deformation under load, while electrical and thermal conductivity determine how heat is generated and removed from the contact zone. Surface behavior governs interaction with molten material and spatter.
This article presents measured production results from two industrial welding environments. The first case examines electrode behavior in flash butt welding, where current and mechanical load define performance. The second case examines fixture components in a robotic welding cell, where thermal exposure and spatter interaction govern maintenance requirements. In each case, a change in material properties led to measurable changes in maintenance frequency and production continuity. These results provide a production-based reference for evaluating material selection prior to RFQ.
For a more comprehensive look at the role of High-Conductivity Alloys see our technical paper
**["Performance and Wear Mechanisms of High-Conductivity Alloys in Resistance Welding"](https://academy.ampcometal.com/landing-page-resistance-welding-2026?utm_source=AM_Collateral&utm_medium=Blog&utm_campaign=2026+-+Resistance+Welding&webInteractiveId=571881834857&webInteractiveContentId=217532233581&containerType=EMBEDDED&campaignId=762e8e18-a359-4b17-bbd7-30f399007242&pageUrl=https%3A%2F%2F5331421.hubspotpreview-na1.com%2F_hcms%2Fpreview%2Fpreview-interactive%3FpreviewInteractiveId%3D217532233581%26_preview%3Dtrue%26portalId%3D5331421%26preview_key%3DDWlQWepN%26tc_deviceCategory%3Ddesktop&portalId=5331421&hsLang=en)**.
[](https://academy.ampcometal.com/hs/cta/wi/redirect?encryptedPayload=AVxigLLIi9NtivhbDuZ5cI9LlFRTFSaUqEmkIiYiNSkCatT7uR2BeUb6Te0ep5wN0hKlkjjRvRm4CKOxgxCk7D6I63EcdxIT3EVRuS3vmR0DJcQoophp0QOmCvy6NCzQMQsnAtOdKFy12IhWy%2FOaSbLf%2BU0EyH1W6m%2B8tAHb5HTRFPmVBzgFo7hmi7kvHHGuedku9ptqEQRl%2Fu5NqjTLDpzAG9EAQr5olyMaT7PXnIXoD6JYCfRYkGgz%2FWvYWWpOVzaOLSsVzfApv39lUUvQ4gNEp2rRCsrFDlMKK8qeUwWTvKRtxXw9rbjlegQZa5OY4ingSWYgfsFsIKbRVmSfqaBql%2F6NrdSCQuMysFg%3D&webInteractiveContentId=217532233581&portalId=5331421&hsLang=en)
### Key Takeaways
- In flash butt welding of band saw blades, replacing CuAl10Ni with [AMPCO® 18](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-18/?utm_source=AMPCO_Academy&utm_medium=blog&utm_campaign=2026_Resistance_Welding&utm_id=092026#product-description) reduced reprofiling frequency by 50%, while maintaining equivalent stroke life and reducing procurement (~10%) and inventory (~90%) costs.
- In robotic welding environments, replacing EN31 fixture components with AMPCOLOY® Mylar eliminated cleaning operations during the observed production period, recovering approximately 40 minutes/day and enabling up to 325 additional jobs/month.
- Increased hardness reduces deformation under mechanical load, while higher electrical and thermal conductivity improve heat dissipation and limit temperature-driven softening.
- Surface stability in copper-based alloys limits weld spatter adhesion, reducing maintenance intervention and associated downtime in welding fixtures.
- Material selection directly influences maintenance interval, process stability, and production throughput under defined operating conditions.
### Case 1 – Flash Butt Welding: Electrode Performance Under High Load
The application involves a band saw blade manufacturer operating in India as a subsidiary of a German machine producer supplying sawing solutions to engineering industries. The company manufactures saw blades using flash butt welding and supports its customers through integrated engineering and service capabilities. Production requirements include consistent weld quality, controlled maintenance intervals, and stable supply of critical welding components.
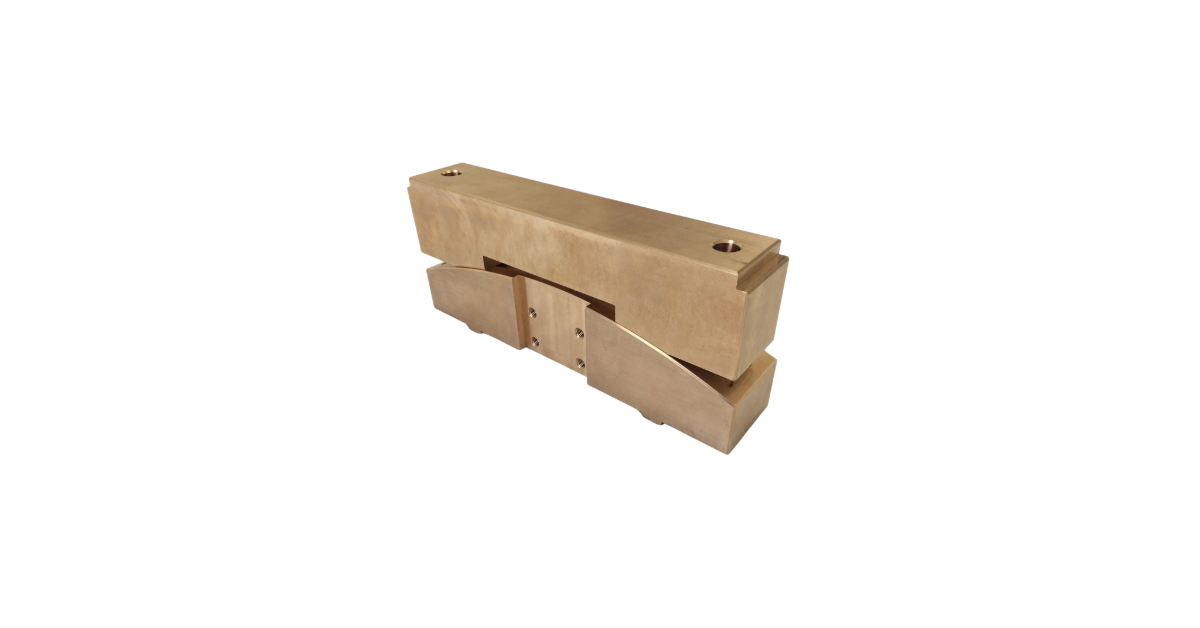
In this environment, RWMA Class 5 electrodes are used for flash butt welding of saw blades. These electrodes operate under high electrical current, typically in the range of 40–100 kA, combined with significant clamping force. The electrode functions as both a current carrier and a load-bearing element, requiring stable geometry and thermal behavior throughout repeated welding cycles.
The initial electrode material was CuAl10Ni, sourced from the parent company in Germany. While the material met baseline performance requirements, the company identified several operational constraints associated with its use:
- Procurement lead times were extended and not fixed
- Inventory levels had to be maintained at approximately 20 sets to ensure continuity
- Inventory carrying costs increased due to imported material and associated logistics
- Reprofiling was required every 4 days to restore electrode geometry
The observed reprofiling frequency indicates progressive deformation of the electrode surface under combined thermal and mechanical loading. Changes in contact geometry over time affect current density distribution and require periodic intervention to maintain stable welding conditions.
To address both performance and supply chain constraints, a material substitution was implemented using [AMPCO® 18](https://www.ampcometal.com/products/ampco-aluminum-bronze/ampco-18/?utm_source=AMPCO_Academy&utm_medium=blog&utm_campaign=2026_Resistance_Welding&utm_id=092026#product-description), also classified under RWMA Class 5. This material provides a different balance of mechanical and thermal properties, with hardness of 192 HBW, electrical conductivity of approximately 12% IACS, and thermal conductivity of approximately 63 W/m·K.
These properties represent measurable changes relative to the initial material:
- Hardness increased from 160 HBW to 192 HBW
- Electrical conductivity increased from 8% to 12% IACS
- Thermal conductivity increased from approximately 36 to 63 W/m·K
These changes directly influence deformation behavior and heat transfer at the electrode interface during welding.
#### Measured Production Results
| **Parameter** | **CuAl10Ni** | **AMPCO® 18** | **Observed Effect** |
| --- | --- | --- | --- |
| Hardness | 160 HBW | 192 HBW | Increased deformation resistance |
| Electrical conductivity | 8% IACS | 12% IACS | Improved current flow and heat distribution |
| Thermal conductivity | 36 W/m·K | 63 W/m·K | Improved heat dissipation |
| Life in strokes | ~18,000 | ~18,000 | Equivalent performance |
| Reprofiling interval | 4 days | 6 days | Reduced maintenance frequency |
| Procurement lead time | Not fixed | Scheduled | Stable supply |
| Inventory level | 20 sets | 2 sets | Reduced inventory requirement |
| Procurement cost | Baseline | -10% | Reduced cost |
| Inventory carrying cost | Baseline | -90% | Reduced carrying cost |
The extension of the reprofiling interval from 4 to 6 days reflects a change in how the electrode responds to combined thermal and mechanical loading during operation. With higher hardness and improved heat transfer characteristics, the electrode maintains its contact geometry more consistently over repeated cycles, reducing the rate at which deformation accumulates.
This change does not alter the total stroke life, which remains at approximately 18,000 strokes. The difference lies in the distribution of wear over time. Degradation progresses at a slower and more controlled rate, allowing the electrode to operate within acceptable geometric limits for longer periods between maintenance interventions.
At the same time, improved thermal behavior reduces the duration and intensity of temperature exposure at the contact interface. This supports retention of mechanical strength during operation and contributes to the stability of contact conditions throughout the welding cycle.
These effects extend beyond electrode performance alone. The increased predictability of maintenance intervals enables alignment of procurement and inventory planning with actual consumption. With defined delivery schedules and reduced variability in electrode usage, inventory requirements were reduced from 20 sets to 2 sets, lowering carrying costs and simplifying supply chain management.
The result is a more stable production system in which electrode behavior, maintenance planning, and supply logistics operate within a defined and predictable range under unchanged welding parameters.
### Case 2 – Robotic Welding Fixture: Surface Stability and Spatter Interaction
Jay Bharat Maruti Ltd., a Tier 1 supplier to Maruti Suzuki India Ltd., manufactures automotive components including body-in-white (BIW) structures, chassis systems, and safety-critical assemblies. Their production facility in Gurugram, Haryana operates highly automated robotic welding lines designed for consistent, high-volume output.
In one of their robotic MIG welding cells used for crossmember production, fixture resting blocks (mylars) were positioned in close proximity to the welding zone. These components are responsible for maintaining part positioning and dimensional accuracy throughout the welding cycle. Their surface condition directly influences process stability and repeatability.
The welding station operated under the following conditions:
- **Welding process:** Robotic MIG welding
- **Production rate:** 150 parts/shift (300 parts/day)
- **Cycle time:** 192 seconds per part
- **Total welding length:** ~700 mm per component
- **Welding wire:** 1.2 mm Er70C-6M
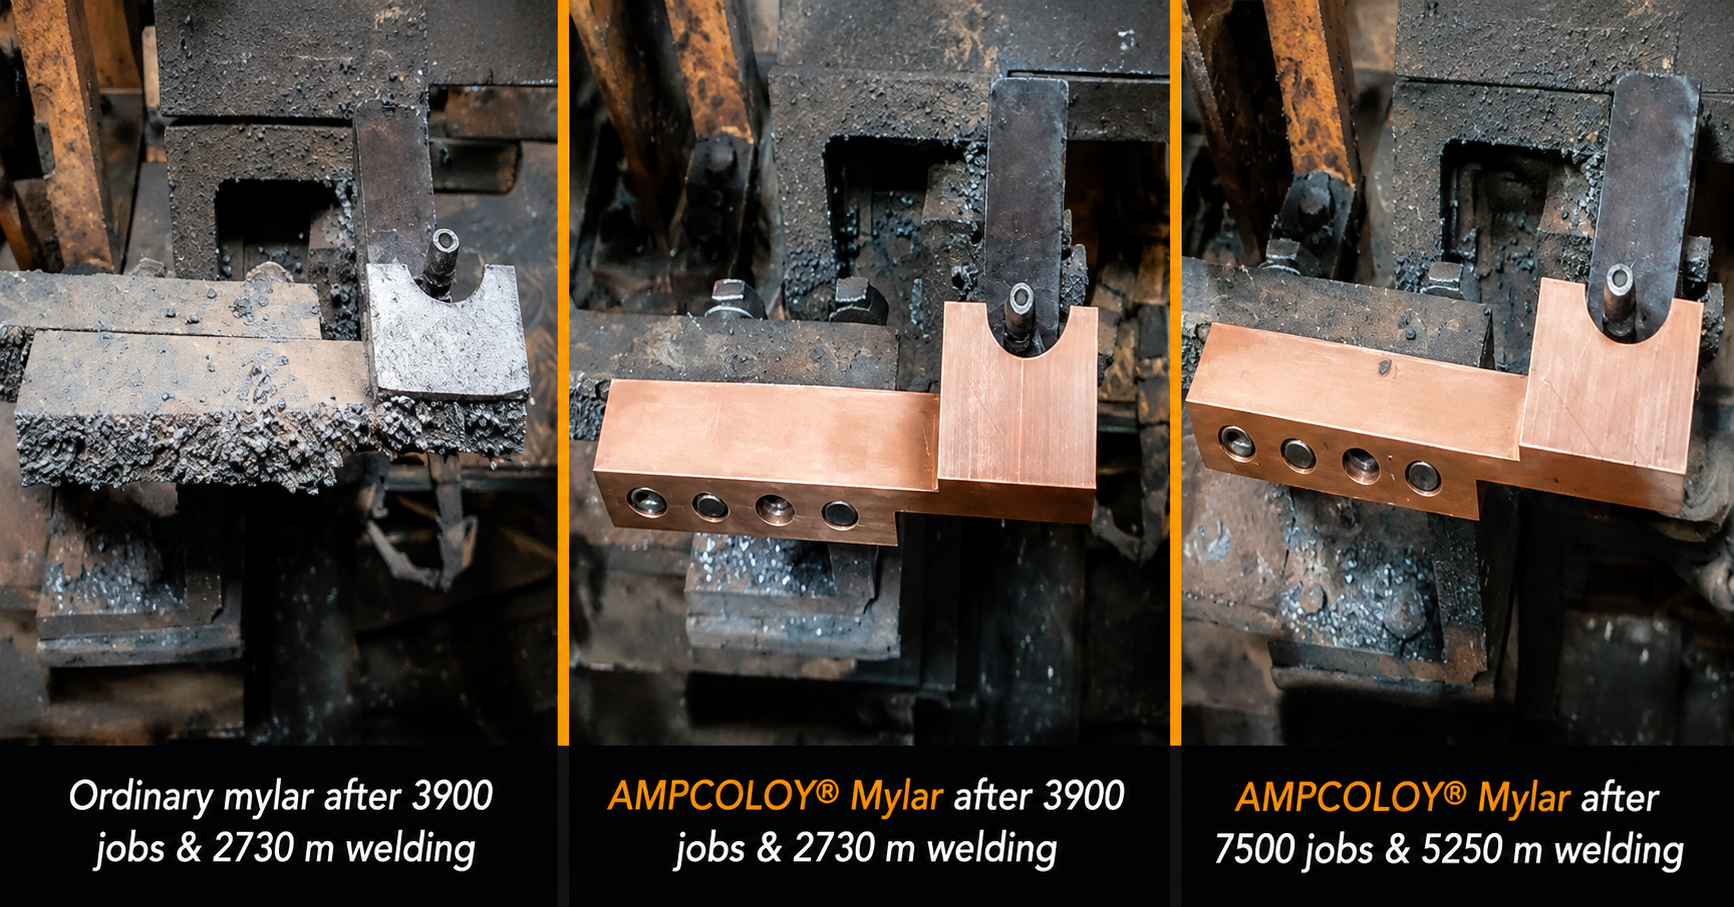
Under these conditions, significant spatter generation occurred during welding. The existing fixture material, EN31 steel (heat-treated and black oxidized), accumulated spatter rapidly on the resting surfaces. This accumulation altered the contact condition between the component and the fixture, affecting positioning accuracy and requiring frequent cleaning.
Cleaning operations were required approximately every 3 to 4 production cycles, with each cleaning event taking approximately 2 minutes. In addition, a comprehensive cleaning operation was performed at the end of each shift, requiring 15 to 20 minutes of manual intervention using chiselling and mechanical removal methods.
This resulted in:
- Approximately 20 cleaning cycles per shift
- A minimum of 20 minutes cleaning time per shift, plus 10–20 minutes at shift end
- Progressive surface damage to the mylar due to mechanical cleaning
- Increased maintenance effort and replacement frequency
The observed limitation was not related to mechanical load or deformation, but to surface interaction with molten spatter and thermal exposure, which drove maintenance requirements and reduced available production time.
To address this, AMPCOLOY® Mylar, a high-conductivity copper alloy, was introduced as a replacement material. The material was selected based on its thermal behavior and surface stability under welding conditions, allowing it to be positioned near the welding arc without requiring coatings or anti-spatter treatments.
#### Measured Production Results
| **Parameter** | **EN31** | **AMPCOLOY® Mylar** | **Observed Effect** |
| --- | --- | --- | --- |
| Cleaning frequency | ~20/shift | 0 | Eliminated during test period |
| Cleaning time | ~40 min/day | 0 | Recovered production time |
| Monthly time loss | ~17.3 hours | 0 | Increased availability |
| Additional production capacity | Baseline | +12 jobs/day | Increased throughput |
| Monthly output increase | Baseline | +325 jobs/month | Increased throughput |
The elimination of cleaning operations was observed over a one-month trial period under stable production conditions.
The performance change is associated with the interaction between thermal behavior and surface condition. The higher thermal conductivity of the copper-based alloy reduces localized heat concentration at the fixture interface, limiting the tendency for molten spatter to adhere and accumulate.
The material maintains a stable surface condition throughout operation, allowing it to function without the need for coatings, sprays, or repeated cleaning. The absence of spatter buildup preserves the geometry of the resting surface, maintaining consistent part positioning and eliminating variation introduced by surface degradation.
The measured outcome is a direct conversion of maintenance time into production time. The removal of cleaning cycles increases equipment availability and enables additional output under the same operating parameters.
### What These Results Demonstrate in Production
The two cases represent different operating conditions, with distinct dominant mechanisms influencing performance. In flash butt welding, deformation under load combined with thermal exposure determines electrode behavior. In robotic welding fixtures, surface interaction with molten material defines maintenance requirements.
In both environments, material properties govern how degradation develops during operation.
- Hardness influences the rate of geometry change under load.
- Electrical and thermal conductivity determine how heat is distributed and removed.
- Surface characteristics define interaction with molten material and spatter.
These property-driven effects act within fixed welding parameters. Current, force, and cycle time remain unchanged, while the material response determines how these conditions evolve during repeated cycles.
The measured outcomes show that performance is expressed through maintenance interval and process continuity. Extended reprofiling intervals and elimination of cleaning cycles indicate that geometry, thermal behavior, and surface condition remain stable over longer operating periods.
Material selection therefore defines the rate at which electrode geometry, temperature distribution, and surface condition change during production. This rate directly determines how frequently intervention is required to maintain stable and continuous operation.
### From Case Evidence to Engineering Decision
Production data such as these provide a direct basis for evaluating material selection in similar environments. When maintenance frequency increases or process conditions drift under stable operating parameters, material behavior becomes a defining factor in performance.
Reprofiling intervals, cleaning frequency, and thermal stability reflect how material properties interact with current, force, and exposure conditions. When these indicators change, the underlying material response is no longer aligned with the operating environment.
In such conditions, adjusting process parameters alone does not address the source of variation. Material substitution becomes a defined engineering step.
The following material characteristics are representative of the property ranges involved in the two applications:
| **Property** | **AMPCO® 18** | **AMPCOLOY® Mylar** | **Functional Role** |
| --- | --- | --- | --- |
| Hardness (HBW) | ~179–194 HBW | Typically \>150 HBW (application-dependent) | Controls resistance to deformation and geometry stability |
| Electrical conductivity (% IACS) | ~12–14% IACS | High (typically 50%+ IACS range) | Defines current flow and heat generation behavior |
| Thermal conductivity (W/m·K) | ~63 W/m·K | High (typically \>200 W/m·K range) | Governs heat extraction and surface temperature control |
| Surface behavior | Wear-resistant, non-galling | High resistance to spatter adhesion | Defines interaction with molten material and surface degradation |
For decision-making, the relevant step is to align these properties with the dominant constraint in the application. When maintenance frequency increases under stable welding parameters, the material response defines the operating limit of the process. In such cases, material selection should be evaluated in terms of hardness, conductivity, and surface behavior relative to the observed degradation mechanism.
The cases presented show that adjusting these properties changes how wear and degradation develop over time, which directly affects maintenance planning and production continuity. The decision to substitute material is, therefore, based on whether the current material maintains geometry, thermal stability, and surface condition within the required operating interval.
### Discuss Your Application with AMPCO METAL
For evaluation of electrode and welding-line material performance under your specific production conditions, the AMPCO METAL technical team can review your welding parameters, base materials, and current component specifications.
Application-specific discussion allows material properties to be aligned with operating conditions, supporting selection decisions and implementation planning in production environments. Contact us below.
[](https://academy.ampcometal.com/hs/cta/wi/redirect?encryptedPayload=AVxigLImSHlJKhRegQ3j%2FTNQbb65bVrIjkR2xtF9YgEhfAjljNqyqbKy7PXRjuHy4Awp%2FhIB3L66M%2FHA%2FmGl%2FsTR9%2BTr996%2F85kYRaCGLPkmsPn2cvvCgUj%2BoMeXejp12Uh9CYFd%2BThNIYkd9uVKoWJNCpVmSGr72BXZwL5O2%2BNKczjiuusL8%2B1p3wgk0rAmAGm342FIW%2FiLBSp%2FylWnBov%2BpCDRDTUdWdZs%2FtaA81aVf2Q60SGH7YukaOAsWfY49nNWGn8Xsdi6BNDL04viq5senub5Vg%3D%3D&webInteractiveContentId=220187818306&portalId=5331421&hsLang=en)
[](https://cta-redirect.hubspot.com/cta/redirect/5331421/8da01823-dd9b-42be-91b8-c4efd4d4c1ea)
-
-
-
-
- [Terms of use](https://www.ampcometal.com/terms-of-use/)
- [Privacy](https://www.ampcometal.com/privacy/)
- [Links](https://www.ampcometal.com/links/)
- [Sitemap](https://www.ampcometal.com/sitemap/)
- [Code of ethics and conduct](https://www.ampcometal.com/documents/CODE-of-ETHICS-and-CONDUCT.pdf)
© 2026 AMPCO METAL